Continuous sand mixers
Single-arm and double-arm no-bake mixers with high-speed mixing trough, metered resin and hardener pumps, and recipe control on HMI. Batch mixers for small jobbing shops.
- 6 TPH
- 10 TPH
- 15 TPH
- 20 TPH
- 35 TPH turbo
- ▶ See photo
No-bake sand foundry equipment · Ahmedabad, India
Engineering-first no-bake sand plant equipment, sized for today and upgradeable tomorrow. THRAEX CO & JEK design and build continuous mixers, knockout machines, vibrating elevators, sand reclamation, cooler classifiers and pneumatic conveying in our Bakrol works, Ahmedabad, and commission them at your foundry.
Equipment range
Each machine is sized from your casting weight, pouring schedule and sand-to-metal ratio. Standard models below; special sizes are designed to order.
Single-arm and double-arm no-bake mixers with high-speed mixing trough, metered resin and hardener pumps, and recipe control on HMI. Batch mixers for small jobbing shops.
Vibratory knockout grids that separate casting from mould and break down lumps. Heavy fabricated decks, twin unbalanced motors, isolated on springs.
Mechanical attrition units and secondary scrubbers that strip spent binder from the grain, plus 3 TPH thermal reclamation for low LOI and reuse in cores.
Fluidised-bed coolers with water-cooled tube bundles bring reclaimed sand to within a few degrees of ambient and remove fines, so the mixer sees consistent sand.
Dense-phase pressure vessel transporters that move sand to storage silos with low grain breakage and low line wear. Bins, silos and level controls supplied.
Roller conveyor and carousel mould loops, flip and rollover moulding machines, compaction tables, mould manipulators and rail transfer cars for large boxes.
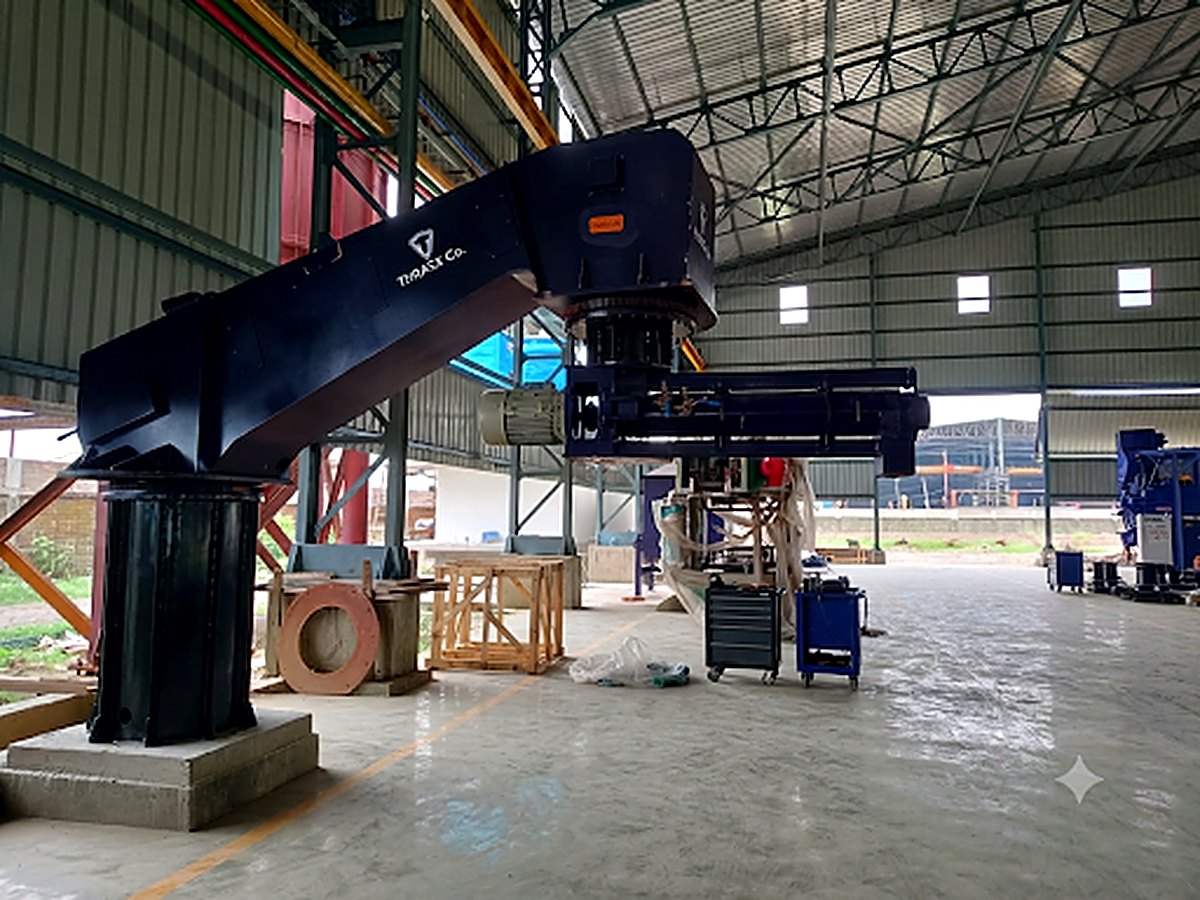
Continuous sand mixers · N-MIX series
A heavy column with slewing ring carries the primary and mixing arms, so one mixer covers every mould on the floor. Resin and hardener are metered into a high-speed trough for even coating at every flow rate.
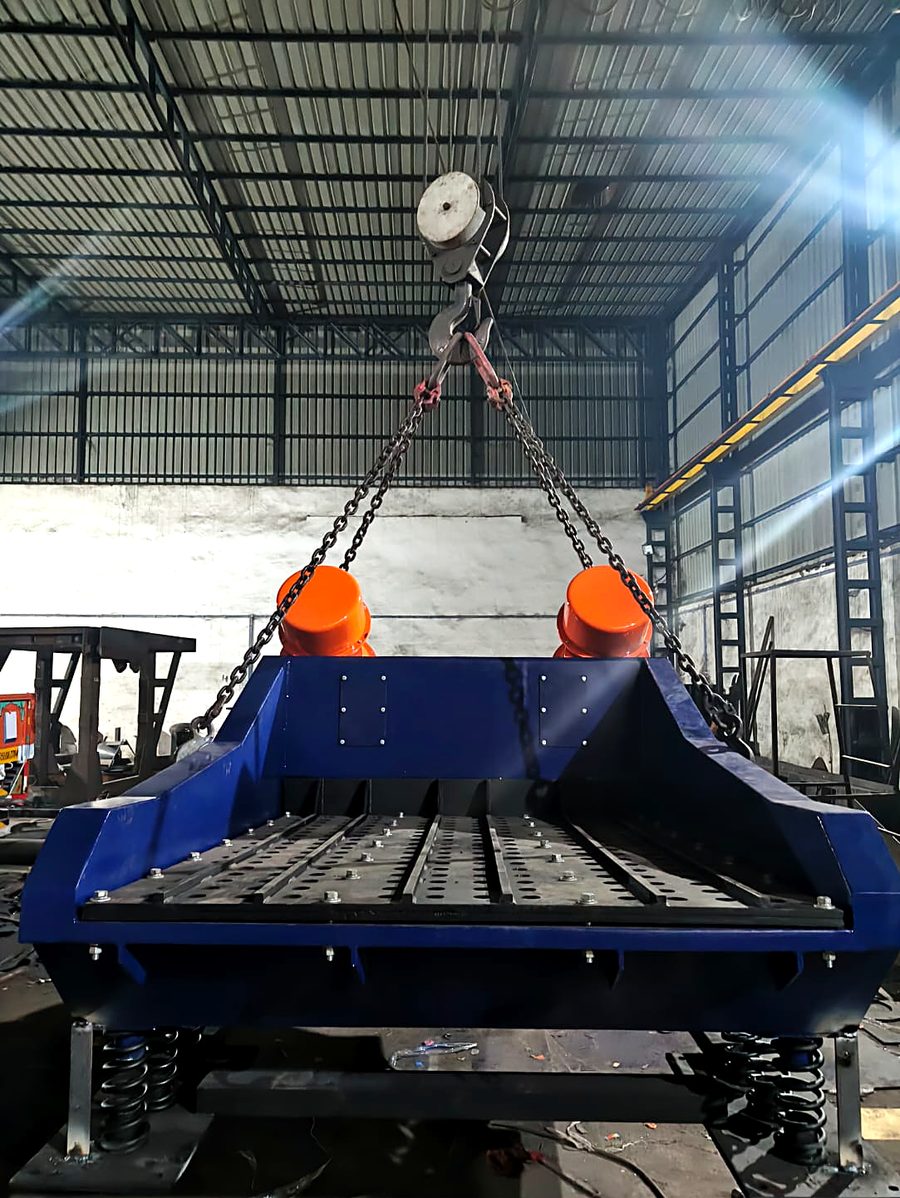
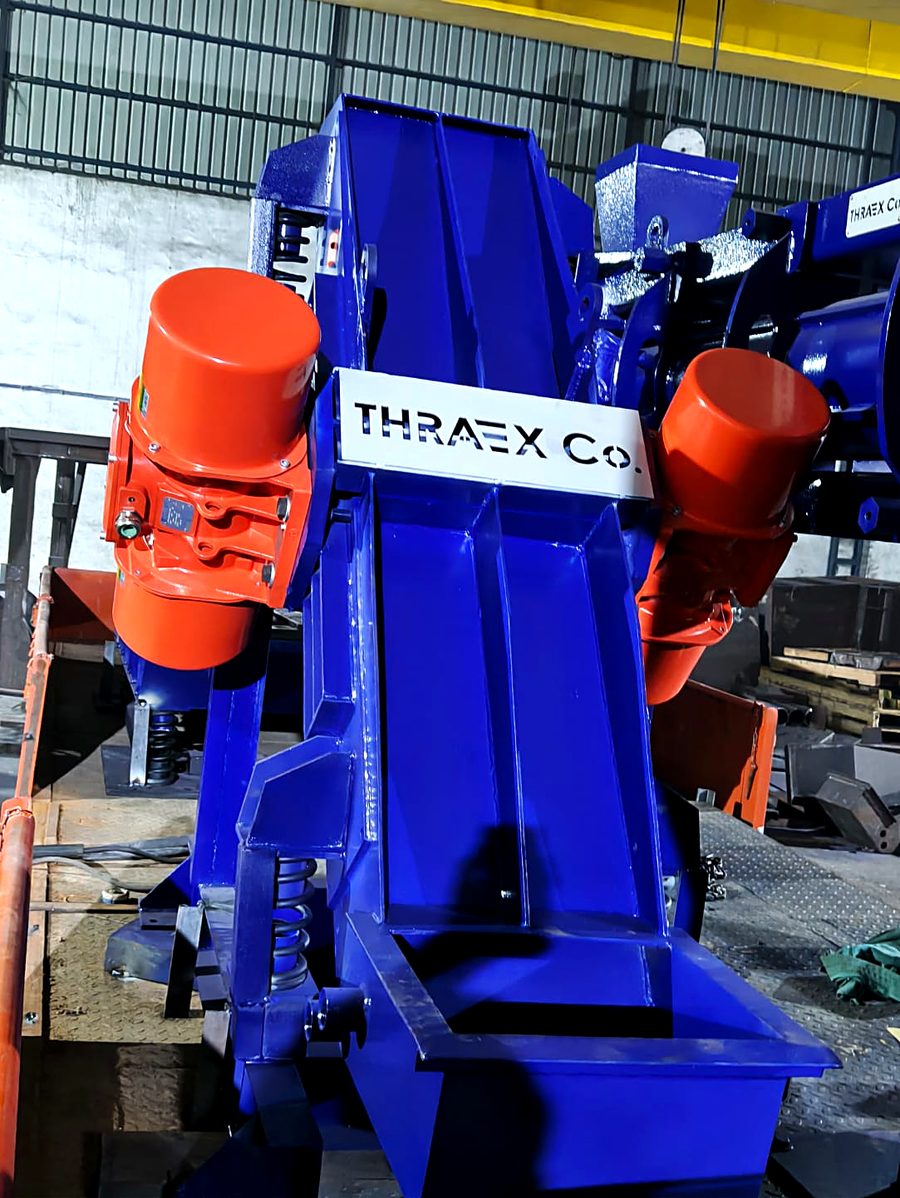
No-bake sand reclamation · Sigma LL series
A complete mechanical reclamation line, assembled and trial-run at our works before dispatch. Spent moulds go in at the knockout; clean, cooled sand comes out ready for the mixer.
SIGMA LL6 – LL15Low-level knockout & attrition unitOLI (Italy) vibrating motors, factor of safety 1.3, 6–15 TPHVIBRATING ELEVATORPitless vibrating elevatorNo civil pit; service at grade level; dust classified out without losing reusable sandSIGMA CC + BLOWERFluidised-bed cooler classifierBaffle-plate cooling bank, high/low level sensors, RTD check on outlet sand temperaturePLC PANELControl panelsWired and tested with the machines before dispatchIn operation
The same line at work in a customer foundry. Twin vibrating motors shake out hot moulds on the spring-mounted deck, and the broken sand flows straight into the vibrating elevator for cooling and reuse.
Smart controls · Industry 4.0
Every N-MIX mixer is controlled from a Mitsubishi PLC and HMI built for the shop floor. Try the interactive version below: start the guided demo and watch the HMI load a recipe, start the mixer, handle a fault and report the shift by itself.
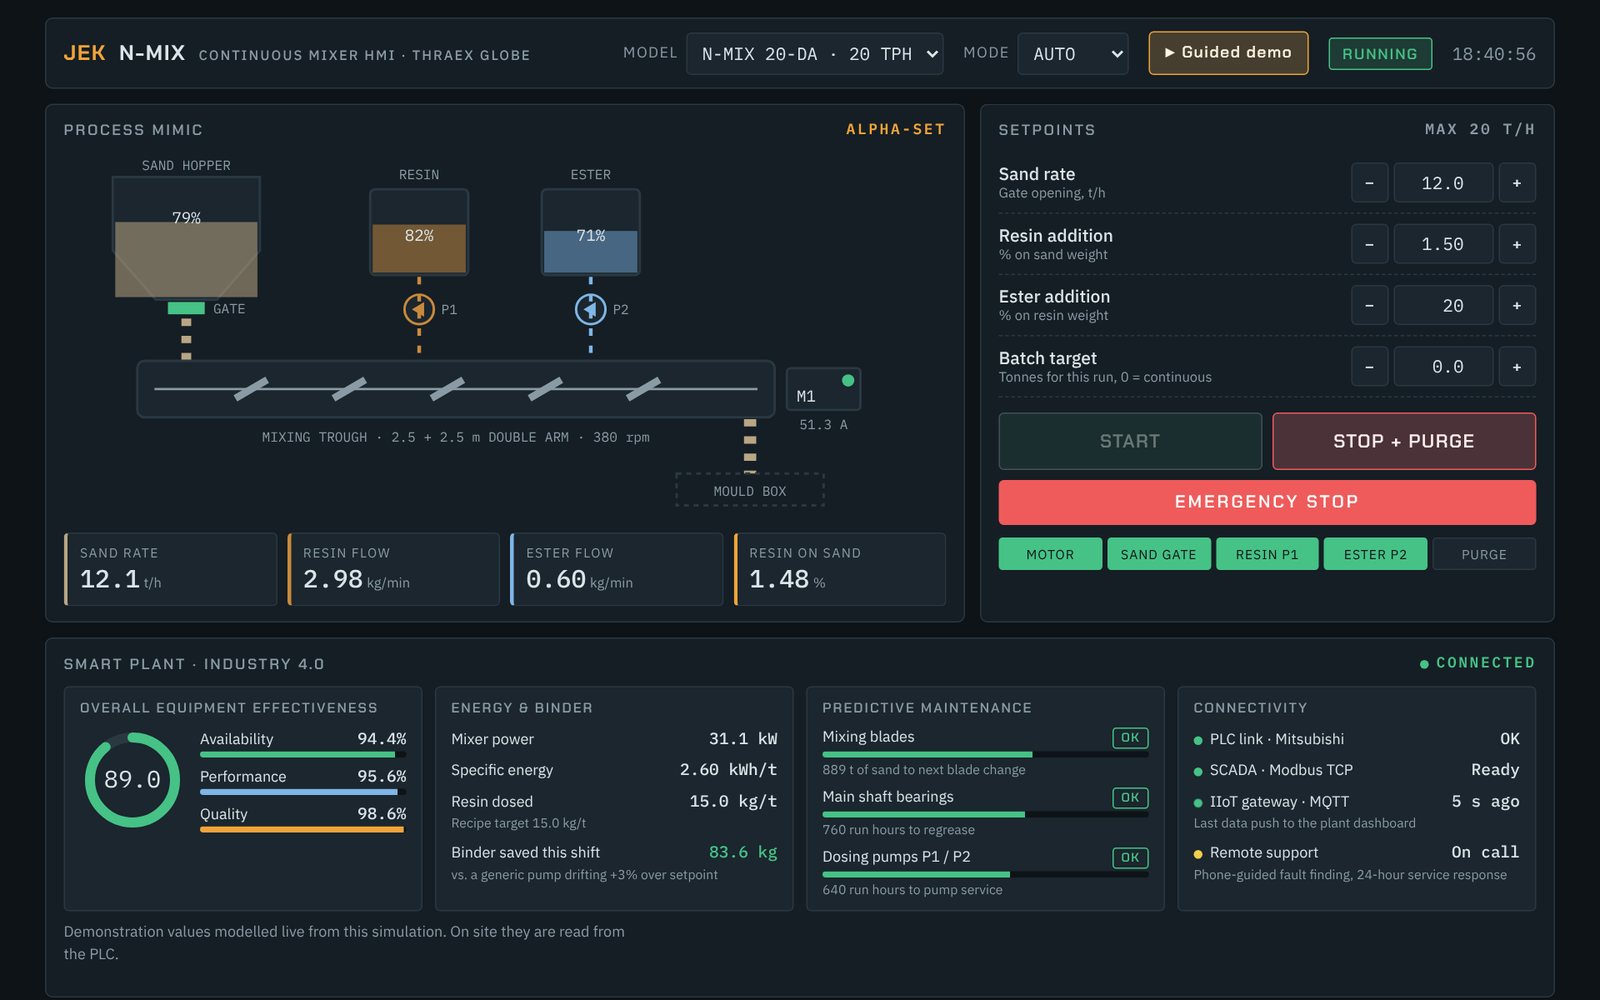 ▶ Start guided demo
Interactive simulation for demonstration · values are modelled, not read from a live PLC
The no-bake sand loop
Sand moves through eight stations and returns to the mixer. When one company builds all of them, capacities match and the controls talk to each other.
Continuous mixer coats sand with resin and hardener at set ratio.
Vibrating table compacts sand around the pattern.
Rollover or flip machine draws the pattern; moulds travel on the loop.
Moulds are poured and cooled on the conveyor or carousel.
Vibratory grid separates casting from mould and breaks lumps.
Attrition removes binder from each grain; dust goes to the collector.
Fluidised bed brings sand to temperature and removes fines.
Pneumatic transporter returns sand to the silo above the mixer.
→ Back to 01. Make-up new sand is added only to replace losses.
Our difference
This is what we put on the table before we talk price.
Every machine, from mixer shaft and paddles to knockout deck, elevator, cooler bank and conveying line, is backed by a design calculation sheet: load, stress, factor of safety, drive sizing and bought-out component selection. Nothing is scaled up by eye from an old drawing.
Critical wear and bought-out parts (motors, vibrators, valves, seals) are listed and stocked as a recommended spares list at the time of supply, not discovered during a breakdown.
Every plant is handed over with an O&M manual and a drawing-referenced part identification document, so your maintenance team can identify, order and replace parts without waiting on us.
Mechanical service support is committed within 24 hours of a call. In continuous casting operations, downtime is measured in hours, not days.
Our PLC and HMI logic is kept deliberately simple, so most electrical faults are diagnosed and fixed through phone-guided troubleshooting without waiting for a site visit.
Inside every plant
| Station | What we fit | Why it matters |
|---|---|---|
| Sand mixing | GemmeCotti Magnetic-drive, seal-less hardener dosing pumps | Precise flow with no shaft seal to leak. Every 1% of binder saved is saved on every mould, every shift. |
| Controls | Mitsubishi PLC + HMI in a dust and solid protected enclosure | Simple recipe screens for shift operators; ladder logic simple enough to diagnose by phone. |
| Knockout | OLI Italy Vibratory motors, factor of safety 1.3 on deck, springs and drive | Consistent shakeout without over-stressing the deck. |
| Vibrating elevator | Pitless design, same OLI drive and FOS 1.3 | No civil pit, simpler install, maintenance at grade level. Fine dust is classified out without carrying away reusable sand. |
| Attrition & cooling | Attrition before cooling; fluidised-bed cooler with intermediate baffle plates, high/low level sensors and RTD at outlet | Sand reaches the mixer at a mouldable, verified temperature every cycle. |
| Conveying | Dense-phase line with butterfly valve and actuator, Y-type NO/NC angle valves, 24 V AC solenoids AIRASMCFesto | Sealed transfer from cooler to main hopper with less sand degradation. |
Head to head
Where the decision-relevant differences actually sit.
| Evaluation point | Typical supplier | THRAEX CO & JEK |
|---|---|---|
| Equipment sizing | Catalogue model closest to stated tonnage | Calculated to your sand, binder and mould-box prerequisites |
| Capacity growth | New machine or parallel line when production rises | Same equipment, same plant, with built-in upgrade headroom (FOS 1.3+) |
| Binder dosing pump | Generic dosing pump, seal-prone | GemmeCotti anti-corrosion, seal-less, precision-flow pump |
| Control philosophy | Complex logic, vendor-dependent for faults | Mitsubishi PLC/HMI, simple logic, dust-protected, phone-diagnosable |
| Knockout & elevator vibration | Unrated or oversized vibrator selection | OLI (Italy) vibrators, FOS 1.3 engineered selection |
| Elevator installation | Civil pit required | Pitless design, simpler install, easier maintenance |
| Cooler classifier control | Manual temperature checks | RTD and level-sensor monitored fluidised-bed cooling |
| Spares & documentation | Spares sourced after a failure | Spares list and part-ID manual handed over at supply |
| Service response | Multi-day site-visit dependency | 24-hour response; electrical faults resolved by phone |
We don't have 20 years of installed base yet; we have five. What we bring instead is a design discipline that treats your growth plan as a specification input, and documentation and service commitments that reduce what you depend on us for after handover.
The full company profile with flow diagrams for mixing, knockout, reclamation and conveying.
Download company profile (PDF)Lost foam casting · turnkey line
A crane-served lost foam line rated for about 8 TPH of dry sand. Pattern shop, moulding and pouring, sand return and dust extraction are designed, built and commissioned by JEK in Ahmedabad. Turnover, moulding and pouring are operator-run, which saves floor space and capital against a fully mechanised loop and still handles mixed flask sizes.
JEK-LFC-PE100Batch pre-expander30 kg/h, bead density 15–50 g/L ±2 %, PLC recipesJEK-LFC-AB3Bead ageing bin2 × 1.5 m³, SS 304 mesh, pneumatic loadingJEK-LFC-HM1512Hydraulic pattern moulding machine1500 × 1200 mm platen, 90–180 s cycleJEK-LFC-PF100Pulse bead-filling tank6 filling guns for thin, complex sectionsJEK-LFC-CT1212Hot-wire cutting table1200 × 1200 mm bedJEK-LFC-CM100Refractory coating mixer100 kg batch, 1.5 kW VFD driveJEK-LFC-DH9Pattern drying heaterHumidity-controlled exhaustJEK-LFC-VT15153-D vibration table1500 × 1500 mm, X-Y-Z compaction, stored recipe per castingJEK-LFC-1512LFC vacuum flask1500 × 1200 × 1300 mm inside, vacuum on bottom and all four wallsJEK-LFC-VP37Vacuum system37 kW water-ring pump, –0.08 MPa, 25 m³/minJEK-LFC-VD3Distributor & pouring hoods3 stations, hoods rated to 600 °CJEK-LFC-SGShakeout grid20 mm plate, Ø16 mm holes, cone hopperJEK-LFC-DC18Pulse-jet bag filter17,800 m³/h, 240 PTFE bags, 30 mg/Nm³ outJEK-LFC-STRSand temperature regulatorReleases sand only at set temperatureJEK-LFC-PSGPneumatic slide gateSand flow adjustable up to 8 TPHJEK-LFC-SHStorage hopper, elevator, screw feederLevel-switch interlocks, 360° slewing feederPLC + HMIOne control panelEnglish HMI (Hindi / Gujarati optional), sequential interlocks, SCADA port, IP54Scope covers design, manufacture, erection supervision, operator training, witnessed trials at our works, full GA and electrical drawings, and a 12-month warranty from commissioning.
Download LFC brochure (PDF) Ask for an LFC offerAbout THRAEX CO & JEK
Five years in business, built around one discipline: technical correctness first, commercial pitch second. Every plant we design starts from calculation sheets, factor-of-safety checks and duty-point selection, not from a catalogue page. We size the machine to your sand chemistry, your tonnage and your production plan for the next five years, not just the next order.
We do not sell a machine for today's tonnage. Every mixer, knockout, elevator, cooler classifier and conveying system carries structural, drive and control headroom, so when you increase mould production the same equipment and the same layout absorb the higher capacity.
Shaft, bearing, motor and structure carry margin, so a capacity increase is a parameter change, not a re-purchase.
Sized from your sand type, binder system, mould box size and target moulds per hour.
Mixer, knockout, elevator, cooler and conveying sized as one system, so no station becomes the bottleneck.
Fewer emergency parts, less binder waste, less downtime: cheaper to own in year 3–5, not only to buy in year 1.
Processes we serve
Questions
Single-arm and double-arm no-bake continuous mixers from 6 TPH to 20 TPH, and turbo mixers up to 35 TPH, for alkaline phenolic (alpha-set), furan and CO₂-silicate binders.
Yes. We supply turnkey plants covering mixer, mould handling, knockout, mechanical or thermal reclamation, cooler classifier, pneumatic conveying, silos and PLC controls, with layout and commissioning.
Yes. We carry out capacity studies and upgrades, for example raising a 5 TPH mechanical reclamation line to 9 TPH, and PLC migrations on existing mixers.
Yes. Our turnkey lost foam line covers the pattern shop (pre-expander, ageing bins, pattern moulding, cutting, coating, drying), 3-D vibration table, vacuum flasks and pump, pouring stations, shakeout, sand cooling and return, and bag-filter dust extraction, about 8 TPH of dry sand from one panel.
Our equipment is designed with a minimum factor of safety of 1.3 and spare drive and control capacity. In most cases a capacity increase is handled on the same machines and the same plant layout, without a replacement or a parallel line.
We commit to mechanical service response within 24 hours of a call. Because our Mitsubishi PLC logic is kept simple, most electrical faults are diagnosed and fixed by phone.
Our works are at 68, Gopal Charan Industrial Estate, Bakrol Bujrang, Ahmedabad, Gujarat, India. We supply foundries across India and overseas.
Enquiry
Share your monthly tonnage and process. We reply with a layout concept and techno-commercial offer.